FibroCeram Materials
High-temperature operations consume enormous energy through furnaces, kilns, reactors, dryers, and heat-treatment lines. They also expose hidden losses. Hot exhaust leaves through stacks, insulation weakens around doors, and burners continue operating during idle periods. These details matter.
This introduction examines how manufacturers can Optimize energy-saving efficiency in high-temperature processes without weakening product quality or worker safety. It focuses on measurable actions, including combustion tuning, waste-heat recovery, improved refractory materials, predictive maintenance, and real-time temperature control. A reliable program begins with verified data. Engineers should compare fuel input, thermal output, production volume, and emissions across comparable operating periods.
Amory Lovins, a respected energy-efficiency expert, stated, “The cheapest energy is the energy you don’t use.” His observation remains practical for industrial heating. A furnace that loses less heat may reduce fuel demand before expensive equipment upgrades begin. Small changes help. Sealing a damaged door can stabilize chamber temperature. Cleaning a heat exchanger can improve recovery performance. Adjusting excess air can prevent unnecessary heating of exhaust gases.
However, no plant is perfectly optimized. A software model may overlook fluctuating feedstock moisture or an operator’s manual adjustment. That limitation deserves attention. Energy savings should therefore be tested through controlled trials, calibrated instruments, and documented results. ISO 50001 principles can support this discipline, while process engineers must confirm that efficiency gains do not create defects, unstable reactions, or unsafe conditions. Real progress is not merely lower fuel consumption. It is dependable thermal performance, verified over time, under real production pressure.
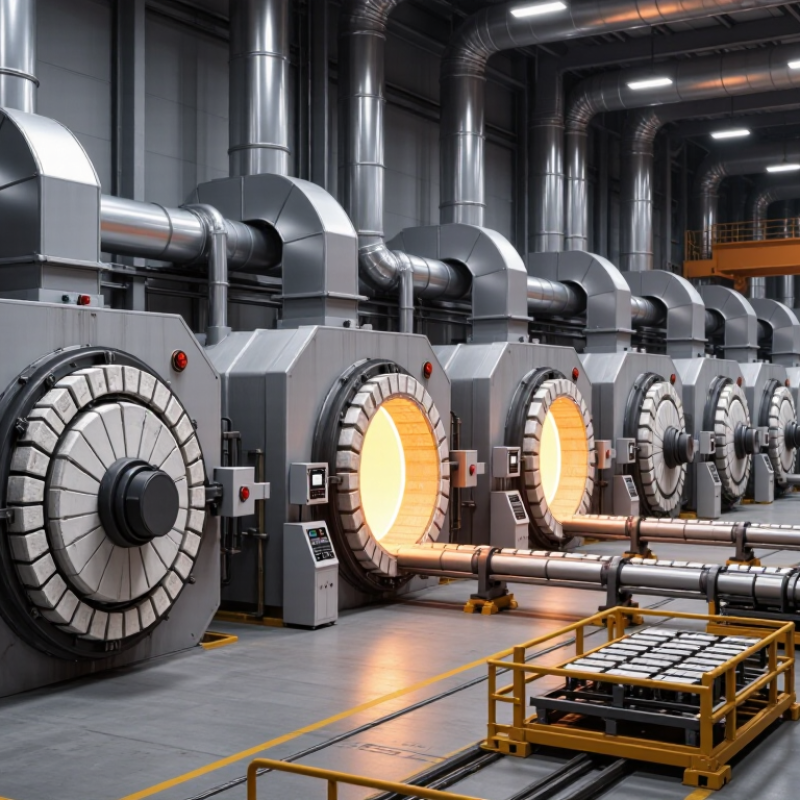
Industry uses about 37% of global final energy, making high-temperature processes a critical optimization target. Furnaces, kilns, reactors, and heat-treatment lines often operate for thousands of hours yearly. Small losses can become significant costs.
A reliable energy baseline begins with clear boundaries. Measure fuel, electricity, production volume, operating hours, and product quality together. Separate startup energy from steady production. Record exhaust temperature, wall temperature, and air leakage during normal shifts. One number is not enough.
In plant assessments, teams often discover that their first baseline is incomplete. A meter may serve several production lines. Maintenance periods may distort monthly data. These details matter. Measure twice.
Normalize energy use by tonnes produced, moisture removed, or batch completed. Compare similar products under similar temperatures. A sudden increase may indicate insulation damage, poor burner adjustment, excessive door opening, or unstable feedstock. Operators should review the data with maintenance engineers, because spreadsheets rarely show the whole process.
Use the baseline to set practical targets, such as reducing energy per tonne by five percent without lowering output quality. Check performance weekly, not only at the end of the quarter. Thermal cameras, calibrated meters, and verified production records improve confidence. Still, every baseline contains assumptions. Review them when equipment, recipes, or operating schedules change. A perfect model is unlikely. A transparent, regularly tested one is more useful.
| Process | Typical Operating Temperature | Primary Energy Demand | Recommended Baseline Metric | Illustrative Energy-Intensity Range | Main Energy-Loss Sources | High-Impact Optimization Actions | Baseline Data Frequency |
|---|---|---|---|---|---|---|---|
| Cement clinker production | Approximately 1,450 °C in the burning zone | Thermal energy for raw-meal calcination and clinker formation | GJ per tonne of clinker | Approximately 3.0–4.5 GJ/t clinker | Preheater and cooler exhaust, kiln shell radiation, false air, incomplete heat recovery | Optimize kiln combustion, reduce false air, improve clinker-cooler heat recovery, and stabilize feed chemistry | Each shift, with monthly normalization |
| Primary steelmaking and reheating | Reheating furnaces commonly operate at approximately 1,100–1,250 °C | Natural gas, electricity, or other thermal energy carriers depending on furnace type | GJ per tonne of crude steel or reheated product | Approximately 0.8–3.0 GJ/t, depending on route and process boundary | Furnace-wall losses, exhaust-gas losses, door openings, scale formation, and low load factor | Use recuperative or regenerative combustion, improve furnace sealing, optimize scheduling, and recover sensible heat | Per heat or production batch |
| Glass melting | Approximately 1,400–1,600 °C in the melting zone | High-temperature fuel combustion and electricity for auxiliary equipment | GJ per tonne of molten glass | Approximately 3.5–8.0 GJ/t, depending on glass type and furnace design | Flue-gas discharge, furnace-wall radiation, batch moisture, air leakage, and inefficient combustion | Increase cullet use where technically suitable, optimize combustion air, improve insulation, and recover flue-gas heat | Hourly monitoring with daily reconciliation |
| Lime calcination | Approximately 900–1,200 °C | Thermal energy for limestone calcination | GJ per tonne of quicklime | Approximately 3.2–5.5 GJ/t quicklime | Excess air, kiln-wall heat loss, uneven feed size, hot-product discharge, and incomplete heat recovery | Control excess oxygen, optimize stone sizing, recover heat from product cooling, and improve kiln insulation | Each production shift |
| Ceramic firing | Approximately 1,000–1,400 °C, depending on product | Thermal energy for drying, firing, and controlled cooling | GJ per tonne of saleable product | Approximately 2.0–6.0 GJ/t, depending on product density and firing cycle | Excess kiln volume, hot-air discharge, poor loading density, kiln leakage, and extended firing cycles | Recover cooling-zone heat, optimize kiln loading, reduce cycle time, control moisture, and improve insulation | Per kiln cycle |
| Aluminium melting and holding | Approximately 660–750 °C for melting and holding | Natural gas, electricity, or both, depending on furnace technology | GJ per tonne of molten aluminium | Approximately 1.0–4.0 GJ/t, depending on charge material and furnace operation | Metal oxidation, furnace-door opening, exhaust losses, refractory losses, and low furnace utilization | Increase recycled-metal charge where quality allows, minimize holding time, control burner air ratio, and recover exhaust heat | Per melt or batch |
| Industrial steam generation | Approximately 150–540 °C for common steam-generation and superheating duties | Fuel or electricity converted into steam for process heating | Fuel input per tonne of steam | Approximately 2.7–3.2 GJ/t of steam, depending on pressure and feedwater conditions | Flue-gas losses, blowdown, steam leaks, condensate loss, poor insulation, and low return temperature | Maximize condensate return, optimize blowdown, repair steam leaks, use economizers, and insulate distribution lines | 15-minute meter data with monthly review |
Industry uses about 37% of global final energy. Furnaces and kilns may operate thousands of hours yearly. Small losses can become major costs. A baseline shows where energy disappears.
Record fuel, electricity, production volume, operating hours, and product quality. Include exhaust temperature, wall temperature, and air leakage. Separate startup energy from steady production. One number is not enough.
Compare energy per tonne, batch, or amount of moisture removed. Use similar products and similar temperatures. Monthly totals can mislead when maintenance interrupts production.
Possible causes include damaged insulation, poor burner adjustment, frequent door opening, or unstable feedstock. Check the equipment directly. Spreadsheets rarely show the whole process.
Review performance weekly. Do not wait for quarterly reports. Use calibrated meters, thermal cameras, and verified production records. Even then, the baseline may contain mistakes.
Practical systems may reduce fuel use by 10–20%. Actual savings can be lower. Fouling, downtime, pressure loss, and poor heat matching reduce performance.
Recovered heat can preheat combustion air, feedstock, process water, or nearby low-temperature operations. The destination must be useful. Otherwise, the system may only heat equipment.
Recuperators heat incoming combustion air continuously. Regenerative systems use ceramic storage media during reversing cycles. Economizers can preheat water. Heat exchangers can serve nearby processes.
Measure exhaust temperature, oxygen levels, flow rate, and operating hours. Check several normal production shifts. A clean-looking stack can still hide large losses.
Dust can block surfaces. Corrosion can damage equipment. A cracked lining can erase savings quietly. An expected 20% reduction might become 8%. The estimate may be wrong. Recheck assumptions after equipment or schedule changes.
Optimizing energy in high-temperature processes begins with a clear understanding of how energy is used. Since industry accounts for approximately 37% of global final energy consumption and process heat represents nearly 70% of industrial energy demand, companies should establish reliable energy baselines and classify heat requirements by temperature, duration, and application. This approach helps identify major losses and prioritize practical improvements.
To optimize energy-saving efficiency in high-temperature processes, facilities can recover waste heat through heat exchangers, preheating systems, or improved thermal integration, potentially reducing fuel consumption by 10–20%. Electrification should also be evaluated, especially where electric resistance heating can achieve efficiency above 90% and low-carbon electricity is available. Performance must be verified continuously by tracking energy intensity, carbon dioxide emissions, exergy efficiency, and payback periods. Combining accurate measurement, heat recovery, suitable electrification, and regular review can reduce operating costs while improving process reliability and environmental performance.